Technical Engineering Blueprint: The Mechanics of Gravity Flow Racks
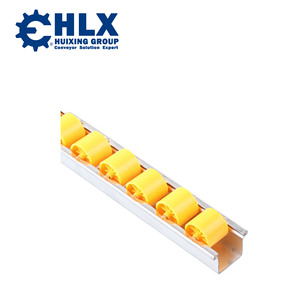
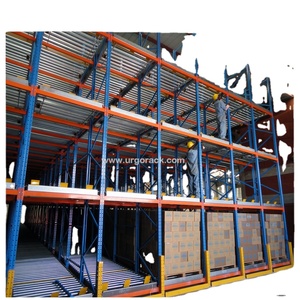
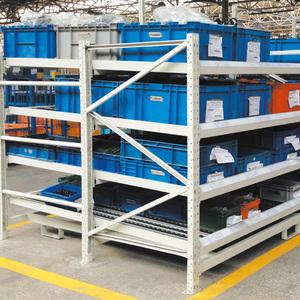
Gravity flow rack systems, commonly referred to as live pallet storage or dynamic carton flow systems, utilize inclined roller tracks to transform static storage into an automated first-in, first-out (FIFO) inventory retrieval matrix. Engineered for operations where inventory turnover speed, high floor cube utilization, and rapid order picking are mission-critical, CE-certified gravity flow racking delivers unparalleled logistics productivity.
At the structural core of a high-performance gravity flow system lies a carefully calculated dynamic slope—typically set between 3.5% and 4.5% (approx. 2.0° to 2.5° decline angle)—which leverages natural gravitational forces to allow loaded pallets or plastic totes to glide seamlessly from the loading (rear) side to the picking (front) face.
Key Kinematic Components in CE Certified Live Storage
Induction-based dynamic friction brake rollers auto-regulate pallet descent speeds to under 0.3 m/s regardless of total pallet weight (ranging from 300kg to 1500kg), preventing excessive kinetic acceleration down long lanes.
Automatic mechanical separation rakes disengage the lead pallet from the line of trailing pallets. This eliminates back-pressure forces on the front pallet, allowing forklift operators to lift lead pallets without binding or drag risks.
Cold-rolled structural steel frames with galvanized or electro-statically applied powder coatings handle intense cyclic loading while resisting micro-deformations in humid or cold-storage environments (-30°C to +40°C).
Technical Specification Matrix: Gravity Flow vs. Alternative Storage
| Racking Architecture | Space Density | Rotation Principle | Brake System Requirement | Forklift Travel Distance | Capital ROI Horizon |
|---|---|---|---|---|---|
| Gravity Flow (Live Storage) | Ultra-High (Up to 85%) | Strict FIFO | Mandatory (Dynamic Brakes) | Low (Dedicated End Aisles) | 12 - 18 Months |
| Selective Pallet Rack | Low (Approx. 40%) | FIFO / LIFO | None | High (Aisle every row) | Standard baseline |
| Push Back Racking | High (Up to 70%) | Strict LIFO | Internal Springs / Carts | Medium (Front face access) | 18 - 24 Months |
| Drive-In Racking | High (Up to 75%) | Strict LIFO | None (Guide Rails) | High (Truck enters rack) | 24+ Months |
CE Certification Requirements & International Safety Standards Compliance
When procuring heavy industrial gravity flow storage racks from international OEM/ODM suppliers, strict adherence to global safety and structural design compliance is non-negotiable. Gravity flow structures store massive cumulative potential energy; uncertified or improperly engineered racks introduce severe operational risks.
Our gravity flow racking systems manufactured in Nanjing carry full CE Marking compliance under the European Machinery Directive and Construction Products Regulation (CPR). Furthermore, structural engineering layouts strictly observe European Standard EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design), FEM 10.2.02 guidelines, and American RMI (Rack Manufacturers Institute) criteria.
Rigorous Structural Verification & Quality Protocols
To provide clear Information Gain and reliable performance verification, every order undergoes standardized non-destructive testing and mill material certification before export dispatch:
- Material Traceability (EN 10204 3.1): High-yield cold-rolled steel coils (Q235B, Q355B grades) are sourced exclusively from tier-1 steel mills, validated with mill test certificates for tensile strength and elongation performance.
- Third-Party Load Capacity Testing: Finite Element Analysis (FEA) computer modeling combined with destructive physical testing verifies beam deflection limits (not exceeding L/200 under full nominal payload) and upright buckling factors.
- Seismic Resistant Design: Custom structural engineering incorporating heavy-duty floor anchor plates, dual-bracing trusses, and upgraded column protectors rated to absorb forklift impact forces in high-seismic active regions.
- Surface Finish Protection: Automated multi-stage wash, iron-phosphate pretreatments, and thermosetting electrostatic powder coating ensure coating thickness of 60–80 microns, passing 500-hour salt spray corrosion resistance tests.
Future Procurement & Technology Trends in Gravity Live Storage (2025–2030)
As global supply chains accelerate their transition toward Industry 4.0 automation, smart warehousing, and green logistics, procurement managers are rethinking dynamic rack specifications. Gravity flow systems are evolving beyond passive structural frames into intelligent, connected fulfillment modules.
Modern flow lanes are increasingly designed with modified entry funnels, photoelectric sensor bracket mounts, and precision stop plates engineered to interface directly with Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs) for unattended loading and retrieval.
Embedded IoT sensors monitor roller rotation speeds, ambient lane temperature, and vibration signatures in cold-storage environments. Real-time telemetry detects roller wear or jammed pallets before operational bottlenecks occur.
Energy costs in refrigerated (-25°C) fulfillment centers drive demand for ultra-dense flow lanes. By reducing warehouse volume requirements per pallet position by up to 60%, gravity flow racking drastically cuts HVAC energy consumption per pallet stored.
Enterprise Advantage: Random Racks Storage Equipment Co., Ltd.
Established in 2004 in the Guli Industry Zone, Jiangning District, Nanjing, Jiangsu, China, Random Racks Storage Equipment Co., Ltd. has grown into a premier global manufacturing facility specializing in custom warehouse racking systems, steel mezzanines, and automated storage solutions.
Spanning two decades of continuous engineering refinement, our factory controls every production phase in-house—from raw steel coil slitting, cold roll-forming of uprights and beams, robotic welding, to automated electrostatic powder coating lines. This total quality control ensures global B2B buyers receive consistent dimensional tolerances, verified structural strength, and reliable export fulfillment.
Our senior engineering team creates comprehensive 2D floor plans and 3D structural CAD layouts tailored to your exact warehouse clear height, floor slab capacity, pallet sizes, and forklift turning radii—completely free of charge prior to order commitment.
We offer full private label branding, custom RAL color powder coatings, specialized lane widths, heavy-duty roller pitches, and tailored packing methods optimized for high-cube ocean container loading.
Exporting to over 60 countries across Europe, North America, Australia, South America, and the Middle East, we provide detailed assembly blueprints, video installation guides, and qualified field supervision on request.
Frequently Asked Questions by Industrial Buyers & Logistics Engineers
Ready to Optimize Your Warehouse FIFO Live Storage?
Submit your warehouse floor plan, clear height, pallet dimensions, and target payload. Our engineering team will deliver a customized 3D/CAD layout, structural calculation, and competitive factory-direct quote within 24 hours.
Inquire Now