Featured Steel Cage & Warehouse Racking Products
Engineered for intense industrial logistics, automated handling systems, and cold-chain resilience. Explore our CE-certified line-up manufactured to rigid European quality metrics.
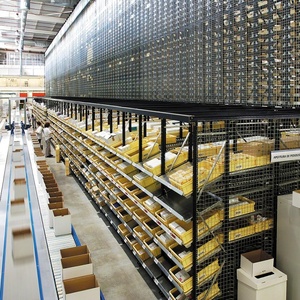
High Efficiency Durable Heavy Duty Adjustable 5-Layer Carton Gravity Flow Rack CE Certified
Precision roller tracks and gravity feed mechanisms tailored for rapid FIFO distribution centers and heavy carton inventory operations.
Inquire Now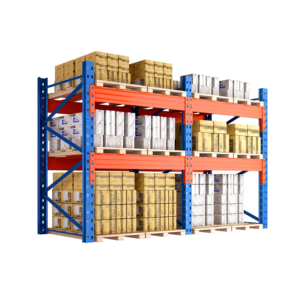
Heavy Duty 5 Steel Warehouse Rack Anti-rust Multi-functional Narrow Aisle Racking
Boltless high-grade structural assembly designed for narrow aisle efficiency, electro-galvanized anti-rust finish, and high load stability.
Inquire Now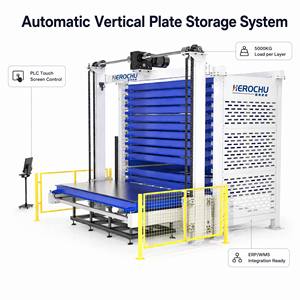
Automatic Vertical Plate Storage System Motorized Drawer ASRS 5000KG Layer
Heavy-duty carbon steel motorized drawer storage system, PLC touch screen interface, ready for WMS/ERP system integration.
Inquire Now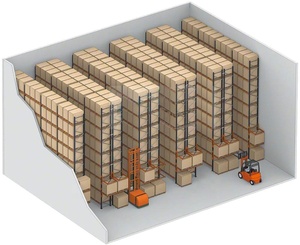
URGO Very Narrow Aisle Pallet Rack / VNA Heavy Duty Racking System
Maximizes vertical cube utilization up to 15 meters height; allows 100% pallet selectivity for guided turret truck operation.
Inquire Now
Selective Heavy Duty Warehouse Storage Rack Shelving System Pallet Racking
Industrial-grade cold-rolled Q235B steel frame with adjustable beam levels, custom load ratings up to 4000kg per level.
Inquire Now
Heavy Duty Racking System Warehouse Storage Tire Pallet Rack & Stackable Cages
Modular automotive tire storage solution; engineered for high-density stackability, safe forklift transport, and powder-coated durability.
Inquire Now
High Density Rack Gravity Flow Racking for Large Load Capacity Storage
Self-energized speed controller rollers for safe continuous pallet descent in high-density cold storage and beverage warehouses.
Inquire Now
NOVA Warehouse Inventory Mezzanine Floor Racking System Industrial Platform
Multi-tier upright-supported mezzanine platform doubling or tripling floor area without costly structural building expansion.
Inquire NowCE Certified Steel Cage Pallets: Engineering Whitepaper & Standards Breakdown
Understanding the Metallurgical Standards, Load Deflection Models, and Certification Protocols Required for Modern Industrial Logistics
In global supply chain logistics, the structural integrity of unit load equipment directly dictates operational throughput, personnel safety, and long-term asset depreciative value. As automated warehouses, high-bay storage racks, and intermodal transport channels become increasingly dense, purchasing directors must look beyond surface aesthetics and evaluate CE certified steel cage pallets, collapsible stillages, and heavy-duty metal containers through rigorous engineering metrics.
Technical Compliance Insight: Under European Norm EN 1090-1 / EN ISO 12100 and the Machinery Directive 2006/42/EC, steel cage pallets utilized in semi-automated and crane-loaded environments must undergo strict Finite Element Analysis (FEA) and dynamic stress testing to verify yield point stability (R_eH ≥ 235 N/mm²) under rated payload limits.
Structural Steel Grades
Fabricated strictly using certified Q235B and Q345B cold-rolled carbon steel. Tensile strength ranges from 370 to 500 MPa, eliminating risk of structural embrittlement during freezing temperatures.
FEA Load Deflection Limits
Engineered for maximum full-load beam and mesh deflection ratios strictly below 1/200th of clear span width under full dynamic movement, preserving safety margins during stack maneuvers.
Surface Protection Profiles
Available in electro-galvanized coating (8–15µm), hot-dip galvanization (60–80µm) according to ISO 1461, or thermosetting epoxy-polyester powder coating for chemical environments.
Mechanical Comparison: Steel Cage Pallets vs. Traditional Timber & Plastic Alternatives
Logistics engineering trials consistently prove that while timber and molded polymer pallets offer lower initial purchase costs, their total cost of ownership (TCO) accelerates rapidly over 36 months due to structural fracture, fire vulnerability, and mechanical deformation under static load pressure.
| Evaluation Parameter | CE Certified Steel Cage Pallets | Industrial Hardwood Pallets | HDPE / PP Plastic Containers |
|---|---|---|---|
| Static Load Capacity | 1,500 kg to 6,000 kg | 800 kg to 1,500 kg | 1,000 kg to 2,500 kg |
| Dynamic Load Capacity | 1,000 kg to 2,500 kg | 500 kg to 1,000 kg | 600 kg to 1,200 kg |
| Stacking Heights (Full Load) | 4 to 6 Levels High | 2 Levels High (Unstable) | 2 to 3 Levels High |
| Fire Safety Compliance | Non-combustible (NFPA Class 1) | High Risk (Combustible) | Melts & Releases Toxins |
| Service Life Cycle | 10+ Years (Repairable) | 1 to 2 Years (High Damage) | 3 to 5 Years (Non-repairable) |
| Recyclability & Scrap Value | 100% Recyclable (High Residual Value) | Negligible / Disposal Cost | Low Thermal Recycling Value |
Future Global Procurement Trends in Steel Cage Pallet Manufacturing
Strategic Shifts Shaping Material Handling Equipment Purchasing for Supply Chain Executives
As enterprise resource management systems (ERP) demand zero-fault traceabilities and carbon-neutral targets, the international procurement landscape for steel wire mesh containers, collapsible stillages, and steel pallets is undergoing structural evolution. Global buyers across North America, Europe, and Australia are prioritizing five core innovation vectors:
1. High Collapse Ratios for Reverse Logistics
Modern procurement strategies favor collapsible wire mesh cages engineered with drop gates and precision hinge assemblies. By achieving a 1:4 or 1:5 reverse transport footprint ratio, international shippers shrink empty container sea freight expenses by up to 75%.
2. RFID & IoT Sensor Integration Hubs
CE-certified steel cages are increasingly customized with flush-mounted sensor pockets for active Bluetooth Low Energy (BLE) or passive UHF RFID transponders, enabling real-time telemetry of temperature, location, and vibration across intermodal nodes.
3. AS/RS Automated Compatibility
Manual handling is rapidly yielding to Autonomous Mobile Robots (AMRs) and Automated Storage and Retrieval Systems (AS/RS). Steel cage feet and bottom runner profiles must adhere to ±1.5mm dimensional tolerance limits to prevent conveyor jams.
Technological Innovations in Steel Cage Pallet Fabrication
How Robotic Automation and Metallurgical Advances Are Redefining Warehouse Durability
Modern steel cage pallet manufacturing has transitioned from labor-intensive manual welding to fully integrated continuous production lines. Tier-1 China racking and container factories utilize high-precision robotic MIG/MAG welding cells, high-frequency coil slitters, and automated powder-coating lines to achieve structural consistency across multi-thousand unit runs.
Robotic Continuous Welds
Eliminates localized structural cold-weld points. Robotic arc positioning ensures uniform penetration depth across wire mesh joints and corner stack feet plates, raising ultimate shear resistance by 35%.
Self-Locking Latch Mechanisms
Advanced drop-gate assemblies now feature ergonomic spring-loaded safety pins. This prevents accidental gate opening when stacked four-high in dynamic seismic zones or during container movement.
Formed Metal Base Beams
Replacing traditional flat bar under-supports with cold-rolled corrugated channels dramatically increases floor load distribution, making cages ideal for rack-beam positioning without sagging.
Enterprise Capabilities: Why Partner with Random Racks / OTS Racking
Two Decades of Specialized Racking & Container Engineering for Global Enterprise Buyers
Founded in 2004 and headquartered in Guli Industry Zone, Jiangning District, Nanjing, Jiangsu, China, Random Racks (OTS Racking Storage Equipment Co., Ltd.) has established itself as an authoritative global manufacturer of warehouse racking systems, heavy-duty steel pallets, and industrial metal containers. Our integrated production facility controls every step of fabrication from raw coil slitting to final surface finishing.
International Code Alignment
All structural designs are evaluated according to AS4084 (Australian Standard for Steel Storage Racking), EN 15512, FEM guidelines, and RMI specifications. Third-party mill certificates and load-test reports are provided per batch.
Free 3D / CAD Engineering Layouts
Our in-house structural engineering team provides complete 3D BIM/CAD layout planning, structural load calculations, and bill of materials (BOM) prior to contract confirmation, ensuring zero field fitment issues.
Custom OEM / ODM Fabrication
From non-standard pallet cage dimensions, specialized drop-gate cutouts, crane lifting lugs, to customized brand RAL powder coatings, we tailor designs around your specific forklift tines and warehouse floor constraints.
Frequently Asked Questions for Overseas Procurement
Technical Clarifications for Engineering Leads, Supply Chain Directors, and Purchasing Agents
How do CE-certified steel cage pallets improve overall warehouse safety and compliance?
CE certification mandates that steel cage pallets comply with structural safety directives such as EN ISO 12100 and Machinery Directive 2006/42/EC. This ensures that load capacity ratings, stacking interlocks, drop-gate latches, and lifting points have passed rigorous mechanical stress and deformation testing. Using certified containers minimizes worker injury risks, prevents sudden structural collapses during dynamic forklift handling, and satisfies stringent occupational safety audits in North America, Europe, and Australasia.
Can steel cage pallets be engineered for automated AS/RS racking systems?
Yes. Automated Storage and Retrieval Systems (AS/RS) require extremely tight manufacturing tolerances to avoid optical sensor errors or conveyor track jams. We manufacture AS/RS-compatible metal cage pallets with base runner tolerances within ±1.5 mm, robotic continuous welds, and specific guide channels designed for stacker crane forks and chain/roller conveyor transport.
What surface treatment is best for cold storage or chemically aggressive environments?
For cold chain storage (down to -30°C) or humid/outdoor applications, Hot-Dip Galvanizing (HDG) according to ISO 1461 is highly recommended. HDG applies a zinc coating layer of 60–80 microns that forms a metallurgical bond with the steel substrate, delivering self-healing anti-corrosion protection for over 15 to 20 years. For dry indoor ambient warehouses, high-durability electrostatic powder coating provides superior cost efficiency and color-coded inventory identification.
What is the typical lead time from design approval to container dispatch?
Standard export orders typically require 15 to 25 manufacturing days after 3D CAD drawing sign-off and deposit receipt. For complex OEM custom projects involving specialized tooling or large volume roll-out contracts, schedules are structured progressively, with first sample confirmation available within 7 to 10 working days.
How do collapsible steel wire cages optimize container sea freight efficiency?
Collapsible wire mesh cages feature heavy-duty perimeter hinges that allow the side walls to fold flat over the base frame when empty. This reduces the height of each unit by 75% to 80%. Consequently, a standard 40ft High Cube container can transport up to 300–400 collapsed units compared to only 70–80 rigid non-foldable cages, slashing sea freight expenditure per unit dramatically.
Does your factory provide third-party load test reports and material mill certs?
Absolutely. Every production run is backed by raw material Mill Test Certificates (MTC) verifying chemical composition and tensile strength (Q235B/Q345B). Furthermore, we provide third-party load test documentation (SGS, TUV, or internal hydraulic rig tests) verifying dynamic loading, static stack weight, and crane hoist capacity.