Engineered High-Density Storage Solutions
Explore our factory-direct mobile racking, VNA, mezzanine, and automated industrial storage matrix built for maximum cube utilization.
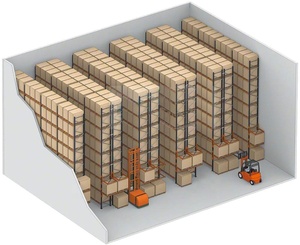
URGO Very Narrow Aisle Pallet Rack / VNA Racking System
Designed for high-bay logistics centers requiring 100% pallet selectivity with aisle widths down to 1.5m to double overall storage capacity.
Inquire Now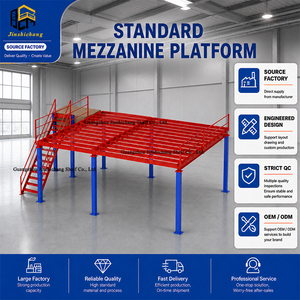
OEM Customized Steel Mezzanine Floor Manufacturer for Warehouse Storage
Heavy-duty multi-tier structural steel platforms designed according to international building codes to double usable clear floor area.
Inquire Now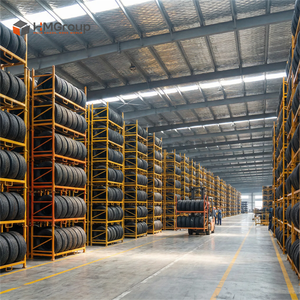
Factory Professional Auto Industry Stackable Metal Steel Tire Storage Rack
Collapsible and stackable 4-high modular storage frames engineered specifically for automotive tires and heavy industrial parts logistics.
Inquire Now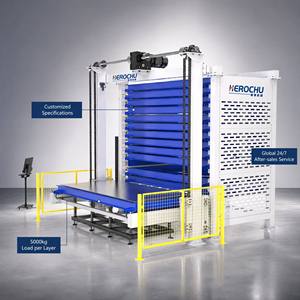
Customizable 5000kg Capacity Multi Tower Smart ASRS Vertical Steel Plate Storage System
Fully automated vertical stacker crane retrieval systems optimized for heavy sheet metal, structural plates, and high-density industrial loads.
Inquire Now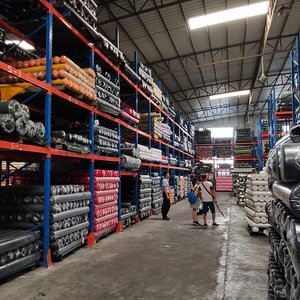
Highly Customizable Free Design Storage Rack for Heavy Duty Loads (1-3 Tons)
Custom roll-formed cold-rolled steel pallet beam racks with customizable frame depths, beam spans, and load ratings up to 3,000kg per level.
Inquire Now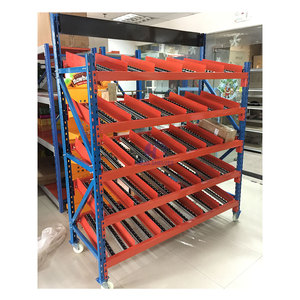
Customized Warehouse Storage Pallet Flow Rack & Gravity Carton Flow Racking
Dynamic roller bed gravity racking systems configured for strict First-In, First-Out (FIFO) inventory rotation in distribution hubs.
Inquire Now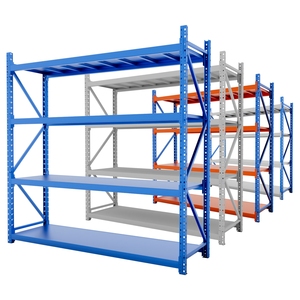
Factory Direct Steel 4-Layer / 500kg Load Heavy Duty Long Span Shelving
Boltless step-beam longspan shelf units compliant with AS4084 guidelines for versatile manual stock picking and archive record management.
Inquire Now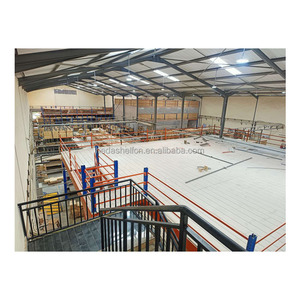
Heavy Duty Steel Large Warehouse Storage Rack Supported Mezzanine Platform
Rack-supported platform architecture using structural uprights as main load-bearing columns for optimal floor space utilization.
Inquire NowMobile Shelving Engineering & Structural Architecture Whitepaper
An authoritative analysis on maximizing volumetric warehouse space with electric mobile racking systems (EMPR).
1. Architectural Fundamentals of Mobile Racking Systems
Industrial mobile shelving systems (often termed Heavy-Duty Mobile Pallet Racking or Electric Mobile Racking) represent the apex of dense storage engineering. Unlike static selective pallet racking—which requires fixed, non-productive operating aisles for every rack row—mobile shelving consolidates multiple storage blocks onto motorized mobile bases mounted on embedded floor steel rails. A single operational aisle is opened electronically on demand, unlocking up to 85% to 90% space utilization efficiency compared to standard 40-45% ratios in traditional setups.
2. Core Structural Engineering Components
Motorized Mobile Bases
Constructed from high-tensile structural steel channels (Q235B / Q355B grade) fitted with precision-machined, polyurethane-coated or forged steel wheels designed to carry point loads exceeding 24 metric tons per carriage assembly.
Dual-Motor Synchro Drives
Direct-drive electric gear motors equipped with soft-start and soft-stop frequency inverters ensure smooth, vibration-free movement, protecting delicate inventory and maintaining frame alignment across long runs.
Multi-Level Safety Curtains
Integrated PLC controllers paired with photoelectric safety barriers, optical infrared distance sensors, and physical impact bumpers automatically halt carriage movement immediately if an object or operator enters the open aisle.
3. Volumetric Efficiency Comparison Matrix
To assist warehouse engineers and procurement heads in making data-backed ROI decisions, the table below outlines structural metrics across mainstream storage configurations:
| Racking Architecture | Aisle Width Requirement | Volumetric Space Utilization | Pallet Selectivity Ratio | Ideal Application Profile |
|---|---|---|---|---|
| Electric Mobile Racking (EMPR) | 3.0m - 3.5m (Single Aisle) | 85% - 90% | 100% Immediate Access | Cold Storage, High Land Cost, Medium-High SKU Count |
| Very Narrow Aisle (VNA) | 1.5m - 1.8m (Fixed Aisles) | 60% - 65% | 100% Immediate Access | High-Bay Fulfillment Centers, Guided Turret Trucks |
| Selective Pallet Racking | 3.2m - 3.8m (Multiple Aisles) | 40% - 45% | 100% Immediate Access | General Logistics, Low Capital Expenditure Needs |
| Radio Shuttle Racking | Deep Lane (No Aisles) | 75% - 80% | LIFO / FIFO (Batch Access) | Bulk Manufacturing, Few SKUs, Mass Beverage Logistics |
Future Procurement Trends in Mobile Storage Systems (2025–2030)
Key technical shifts driving global buyer decisions across European, North American, and Asia-Pacific supply chains.
1. WMS / WCS IoT System Integration
Modern mobile racking systems are no longer isolated mechanical structures. Strategic procurement now mandates PLC units equipped with industrial Ethernet interfaces (Profinet, Modbus TCP) that synchronize directly with Warehouse Management Systems (WMS). Aisles automatically pre-open based on real-time order picking queues, reducing forklift cycle times by up to 35%.
2. Cold Chain Thermal Load Reduction
With global refrigeration energy tariffs escalating, cold storage operators are prioritizing mobile shelving over static racking. By consolidating empty aisle space, cold rooms shrink their cooled volume requirements by up to 45%, delivering dramatic long-term reductions in carbon footprint and operational power overhead.
3. Seismic & Dynamic Load Compliance
International tenders strictly enforce rigorous engineering codes. High-tier mobile systems are designed with moment-resisting upright frames and advanced anchor tie-downs capable of absorbing dynamic lateral inertia forces during rapid carriage movement and seismic events, adhering to FEM 10.2.07 and AS4084 safety thresholds.
Why Source from Our Nanjing Manufacturing Facility?
Over 20 years of continuous innovation, engineering excellence, and international project execution.
Founded in 2004
With over two decades of dedicated R&D and steel fabrication experience, our brand has grown from a regional producer into a global exporter supplying turn-key storage equipment to buyers across 90+ countries.
Structural Standards Compliance
All mobile bases, upright profiles, and longspan beams are engineered in accordance with AS4084 (Australian Standard), FEM 10.2.02, EN 15512, and RMI (USA) design guidelines. Mill certificates and third-party load test reports accompany every shipment.
Free 3D / CAD Engineering Layouts
Our in-house structural engineering team provides custom 3D spatial models, structural load calculations, and full bill of materials (BOM) prior to contract execution, ensuring zero site-assembly surprises.
Ready to Upgrade Your Warehouse Volumetric Efficiency?
Consult with our senior logistics engineers for layout optimization and direct manufacturer quotations.
Inquire NowFrequently Asked Questions (Procurement FAQ)
Key technical and commercial inquiries handled by our engineering design team.
A: Electric mobile racking systems require floor guidance rails embedded into the concrete slab. The concrete slab must meet EN 15620 / DIN 18202 flatness tolerances and have a minimal compressive strength of C25/30 or C30/37 depending on the total wheel load. Our engineers supply detailed rail layout and rebar positioning drawings prior to floor pouring or retrofitting.
A: All our electric mobile bases feature an integrated manual drive release mechanism. In the event of a facility power failure, an operator can disengage the electric gear clutch and easily crank open aisles using a manual mechanical lever. Furthermore, optional Uninterruptible Power Supply (UPS) battery backup modules can be integrated into the main control cabinet.
A: Safety is paramount. Our systems integrate a multi-tiered safety defense framework: (1) Floor-level photoelectric light curtains running the full length of the carriage, (2) Optical access barriers across the front entry, (3) Mechanical emergency-stop buttons on every mobile base console, and (4) Motor overload current sensing units that cut drive power instantly upon unexpected resistance.
A: Yes. We engineer specialized low-temperature mobile storage systems. Electrical control panels are fitted with internal heating elements, wiring uses sub-zero flexible silicone cabling, structural steel components undergo low-temperature impact toughness testing, and gear motors utilize synthetic food-grade low-temperature lubricants suitable for down to -30°C environments.
A: Standard engineering production lead time is typically 20 to 30 days following final CAD drawing sign-off. Components are carefully bundled, labeled, and sea-freight containerized at our Nanjing factory. We provide complete installation instruction manuals, video guidance, and can dispatch commissioning engineers for qualified overseas projects.
Start Your Free Warehouse Layout Consultation
Send us your warehouse dimensions, clear ceiling height, pallet specification, and target load capacity. Our engineering team will return a customized 3D CAD design and factory-direct price quotation within 24 hours.
Inquire Now