Heavy-Duty Storage Systems for High-Density Operations
Explore our CE & ISO-certified pallet racking, structural steel mezzanines, and motorized vertical storage equipment designed to double your warehouse capacity.
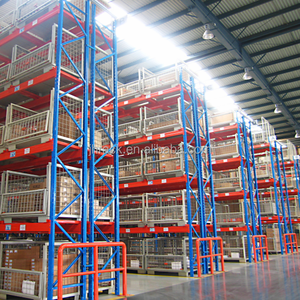
Heavy Duty Metal Warehouse Storage Rack Adjustable Horizontal Shelves For Factory Stacking Racks
Send an Inquiry
Factory Price Customized Steel Medium Duty Mezzanine Floor Rack System Warehouse Multi-Level Storage Office Platform
Send an Inquiry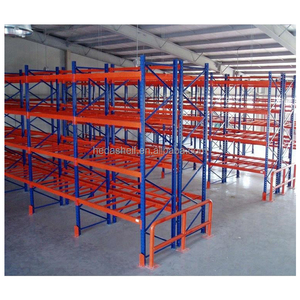
Wide Aisle Pallet Racking Heavy Duty Metal Rack Double Deep Clothes Racking System for Warehouse
Send an Inquiry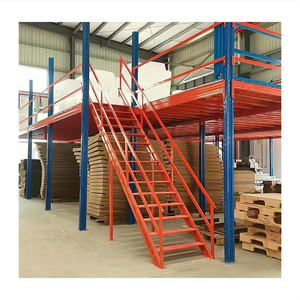
Modular Custom Steel Mezzanine Floor System Multi-Layer Heavy Duty Warehouse Storage Platform 500kg Load Capacity
Send an Inquiry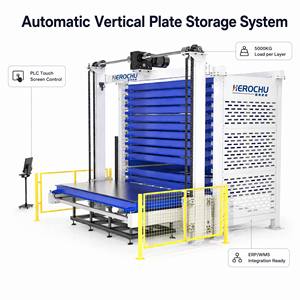
Automatic Vertical Plate Storage System Motorized Drawer Type ASRS Carbon Steel PLC Touch Screen 5000KG Per Layer ERP WMS Ready
Send an Inquiry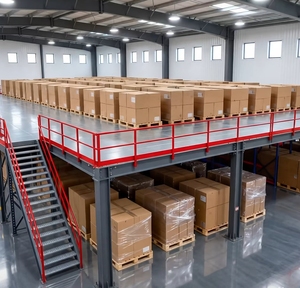
All Our Mezzanine Floors Are Custom-made and Based on Your Wishes and Requirements. We Can Realize Loads up to 2,000 Kg/m2
Send an Inquiry
Factory Double Deep Pallet Racking Warehouse Storage System Light Duty Large Capacity Steel Industrial Warehouse Racks
Send an Inquiry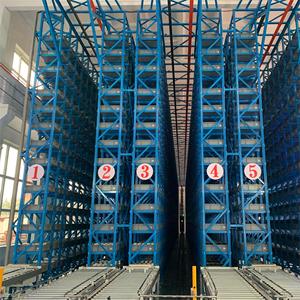
CE Certified Industrial Grade Automatic Storage System ASRS High Efficiency for Auto Parts Manufacturing & Warehouse Logistics
Send an Inquiry1. Executive Summary & Market Mechanics in Kuwait
As Kuwait accelerates its strategic transformation under Kuwait Vision 2035 (NewKuwait), industrial zones such as Shuwaikh Industrial Area, Sabhan, Mina Abdulla, Sulaibiya, and Al Rai are witnessing an unprecedented demand for modern logistics infrastructure. With premium industrial land costs rising across the State of Kuwait, traditional static storage methods—which waste up to 60% of vertical and floor space on fixed aisles—are no longer financially viable for competitive enterprises.
Deploying an engineered Mobile Shelving System (electric motorized heavy-duty mobile racking or manual compact mechanical-assist shelving) provides Kuwaiti business operators with a transformative architectural solution: multiplying warehouse storage capacity by 80% to 100% within the exact same building footprint. As China’s premier manufacturer and direct exporter of heavy-duty storage equipment established in 2004, our systems are tailored specifically to overcome the harsh environmental and operational challenges presented by the Middle Eastern regional climate.
Core Value Proposition for Kuwaiti Buyers: By mounting structural steel racking frames onto floor-guided motorized wheel carriages, mobile racking consolidates multiple operational aisles into a single moving aisle. This achieves up to 85% floor cube utilization, radically cuts cold-storage cooling energy costs in Sulaibiya, and aligns seamlessly with Kuwait Fire Force (KFD) regulations.
2. Engineering Excellence: Mobile Racking System Architecture
Mobile racking systems represent a sophisticated synergy of structural steel engineering, precision mechanical automation, and advanced electrical safety controls. Engineered to EN 15512, FEM 10.2.07, and RMI standards, our high-density mobile storage systems are constructed from Q235B and Q355B cold-rolled steel coils for exceptional strength under heavy payload dynamics.
Precision Recessed Floor Rails
Heavy-duty machined steel rails embedded flush with concrete floor slabs. High-level leveling guarantees smooth movement of multi-ton mobile bases without vibration or derailment risk.
Siemens & Schneider Automation
Driven by Siemens PLC controllers with variable frequency drives (VFD). Smooth soft-start and soft-stop acceleration profiles prevent cargo shifting on upper rack levels.
Multi-Level Safety Curtains
Equipped with photoelectric light barriers, emergency footprint trip bars, and optical distance sensors to ensure complete operator and forklift safety in moving aisles.
Technical Performance Matrix: Mobile vs. Traditional Racking Systems
| Storage System Type | Space Utilization (%) | Pallet Selectivity | Cold Storage Efficiency | Max Payload / Bay | Kuwait Market Applicability |
|---|---|---|---|---|---|
| Electric Heavy-Duty Mobile Racking | 80% – 90% | 100% Direct Access | Maximum (Cuts energy by 40%) | Up to 24,000 kg | High (Cold chain, Industrial hubs) |
| Selective Pallet Racking | 40% – 45% | 100% Direct Access | Poor (High wasted volume) | Up to 15,000 kg | Standard (General low-cost space) |
| Drive-In Racking System | 65% – 75% | Low (LIFO Rotation) | Moderate | Up to 10,000 kg | Bulk homogeneous cargo only |
| Manual Mechanical Mobile Shelving | 85% – 95% | 100% Direct Access | N/A (Ambient office / parts) | 500 kg – 1,500 kg | High (Pharma, Archives, Automotive parts) |
3. Tailored Application Scenarios Across Kuwait’s Economic Zones
Deploying racking equipment in the Arabian Gulf requires extensive localized knowledge regarding ambient environmental extremes, civil construction norms, and regional supply chain patterns.
Sulaibiya Cold Storage & Food Logistics Hubs
In Sulaibiya’s agricultural and frozen food distribution centers, cooling air volume is one of the highest operational costs due to ambient summer temperatures exceeding 50°C. Electric mobile racking eliminates empty aisles, consolidating the cold envelope. This shrinks chilled air requirements by up to 45% while preserving 100% pallet selectivity for strict batch control.
Shuwaikh & Al Rai Commercial & Automotive Parts Depots
Shuwaikh Industrial Area demands maximum storage density per square meter. Our medium and heavy-duty mobile shelving platforms allow auto parts distributors, hardware supply houses, and commercial importers to store tens of thousands of SKUs in compact, dust-protected mechanical carriages with smooth gear-crank handles.
Ahmadi & Mina Abdulla Oil, Gas & Petrochemical Sector
Heavy equipment maintenance depots for KOC/KNPC contractors demand extreme load capacity. Our heavy structural mobile steel carriages support heavy valves, drill bits, pipe fittings, and machinery parts up to 24 metric tons per base unit, fitted with IP65 dust-proof enclosures against Shamal sandstorm intrusion.
4. Extreme Climate Resistance & Surface Finishing Excellence
Kuwait’s coastal proximity (high atmospheric salinity near Shuwaikh Port and Mina Shuaiba) combined with intense heat and fine sand particulates poses severe challenges to structural steel and electric automation. As a trusted China OEM/ODM manufacturer, we integrate rigorous protective measures:
- Automated 6-Stage Pre-Treatment Process: Structural profiles undergo full degreasing, rust removal, zinc phosphating, and nano-ceramic passivation to guarantee superior paint adhesion.
- Heavy Epoxy Powder Coating: Thermosetting pure epoxy-polyester powder is electrostatically applied at 80–110 microns thickness, providing heat, scratch, and salt-spray resistance (passing 500+ hour salt spray testing).
- Thermal Expansion Rails & Sealed Motors: In-floor steel rail channels incorporate thermal expansion gaps to accommodate concrete floor movement during extreme temperature swings, while IP65 sealed gearmotors prevent dust contamination.
5. Kuwait Vision 2035: Strategic Alignment & Industry Growth
Under the National Development Plan, Kuwait is investing heavily in mega logistics projects including the Mubarak Al-Kabeer Port on Bubiyan Island, Northern Gulf Logistics Hubs, and expanded airport cargo terminals. As the nation transitions into a regional financial and trade gateway, warehouse management systems (WMS) and automated storage systems (ASRS / Mobile Racking) are becoming mandatory standards.
Our mobile shelving systems are natively engineered for ERP/WMS integration. Using RFID or barcode scanning, warehouse operators can automatically trigger aisle opening via remote wireless terminals or forklift-mounted tablet screens, accelerating order fulfillment speeds by up to 50%.
6. Why Choose Us as Your China Manufacturing & Export Partner
Since our establishment in 2004, our 35,000m² manufacturing facility in Nanjing, China has delivered thousands of industrial storage projects across 90+ countries. For Kuwaiti logistics companies, procurement managers, and civil contractors, we offer end-to-end direct manufacturer support:
Free 3D CAD & BIM Layouts
Our structural design team provides customized 3D CAD drawings, elevation schematics, and floor slab point-load analysis tailored to your specific warehouse drawings before order confirmation.
Third-Party Load Certification
Every upright frame and beam section undergoes rigorous physical load testing certified by SGS / TÜV Rheinland, validating compliance with international AS4084 and EN structural safety standards.
Export Logistics & Installation Guidance
We provide seaworthy export packaging, container loading optimization, step-by-step assembly manuals, high-definition installation videos, and on-site engineering supervision upon request.
7. Frequently Asked Questions (FAQ) for Kuwait Procurement
Does mobile racking comply with Kuwait Fire Force (KFD) regulations?
Yes. Our electric mobile racking systems feature an automated "Fire Separation Mode." When connected to your facility’s main fire alarm PLC matrix, the system automatically opens all mobile carriages evenly across the room upon smoke detector activation. This provides complete clearance for overhead fire sprinkler systems to penetrate all storage bays.
How do you handle shipping, customs clearance, and delivery to Kuwait ports?
We routinely export directly to Shuwaikh Port and Mina Shuaiba. All products are packed in reinforced, steel-strapped bundles with protective edge wraps to prevent transit damage. We provide full documentation including Certificates of Origin (COO), Commercial Invoices legalized by the Kuwait Embassy/Chamber of Commerce, Packing Lists, and Bill of Lading (B/L).
What floor slab requirements are needed for heavy-duty mobile racking?
Mobile racking requires a level, reinforced concrete floor slab with a minimum thickness of 150mm to 250mm, capable of supporting concentrated wheel loads. We supply exact floor loading calculations and rail installation blueprints so your civil engineering team can prepare the slab or embed rails during concrete pouring.
What is the production and shipping lead time from China to Kuwait?
Standard manufacturing lead time is 20 to 30 days after drawing approval. Ocean freight from Shanghai or Ningbo port to Shuwaikh Port typically takes 22 to 28 days. In total, your complete mobile storage system can be delivered within 50 to 60 days of order placement.
Can manual mechanical mobile shelving be installed in existing offices or archives?
Absolutely. For offices, medical archives, and spare parts rooms, we supply raised modular floor platforms with built-in ramped rail tracks. This eliminates the need to cut or drill into existing concrete floor tiles, allowing rapid installation without structural building modifications.
Transform Your Warehouse Capacity in Kuwait Today
Partner directly with China’s premier racking manufacturer. Send us your warehouse floor plan, clear height, and load requirements for a free engineered 3D CAD layout design and competitive factory-direct quote.